


Metal casting through gasified models is high accuracy of castings for the repair and production of equipment. Creation of your production of castings. Lost Foam Casting Process.
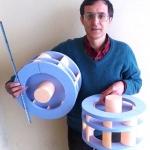
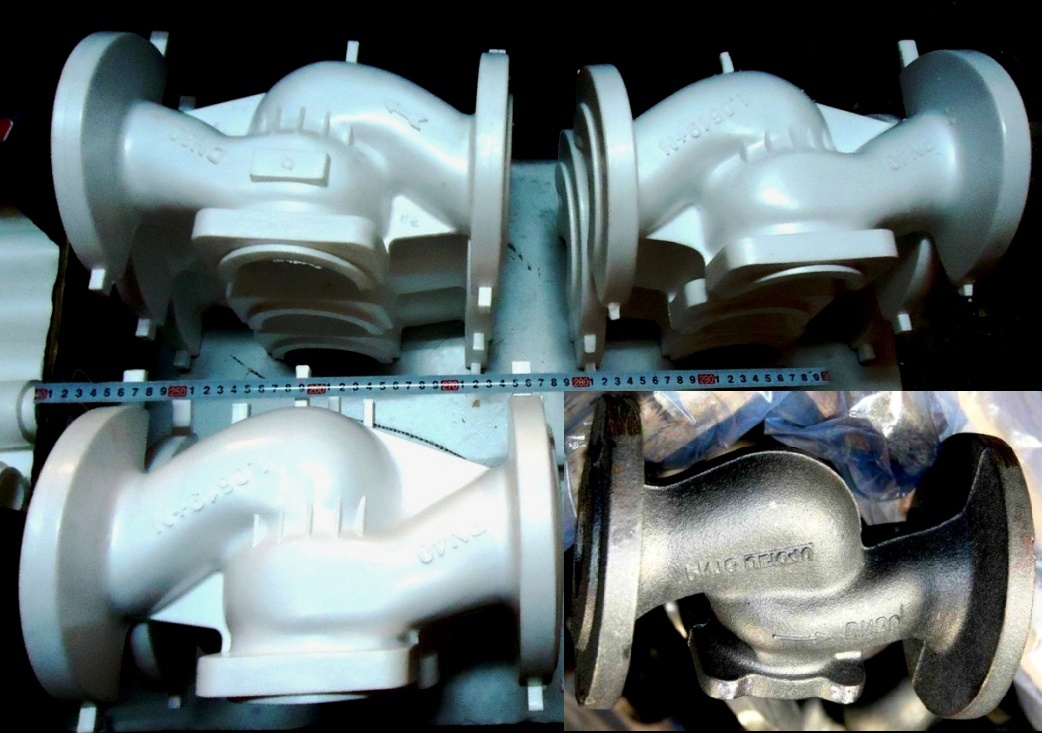
In the foundry, the most accurate castings can be obtained by one -time models. If disposable forms are used in sand forms when casting in sand forms, now they are poured on disposable models from foam. They look like a packaging from a TV, or a one -time food plate, which are massively stamped on machine guns, and the outer walls of the houses are insulated with polystyrene foams.
according to the same technology (as for packaging) for a series of castings, the models are blocked by the peno polystyrene granules into aluminum press forms (multi-seater for small models), followed by foaming granules with heating press forms for about 3 minutes. For one-time and large castings (weighing up to several tons), the models are cut out of foam slabs with heated nichrome wire through templates or on mock-milling machines (3D milling). The model and the casting obtained on it have high accuracy and competitive presentation.
You can freely see the voluminous prototype of the casting in the model, measure its walls, which, with ordinary molding for complex castings with several rods, cannot be made. The model of polystyrene is easier than casting from cast iron by 280 times, take the model in your hands - as if you are holding a void, which then turns into a metal. Typically, the founders are not used to this, stereotypes laid down at the institute, do not allow to see new casting opportunities. Foam models are covered with paint with refractory powder, glued with a gate, covered with dry sand in a box (container) and poured with metal. When pouring, the metal evaporates the model and replaces it with itself. So that the model does not smoke into the workshop when pouring, the gas pump is sucked out of the container-the vacuum supports about half the atmosphere (the household vacuum cleaner gives up to 0.3 atm). There are no stinks of burners, there are no bays according to the form of the shapes (there is no connector) and the displacement of the rods and shapes during assembly, because there are no rods themselves with all the problems of their production and knocking out.
Production sites: model, molding, melting, treatment plants are equipped with simple equipment. The entire molding consists of backfilling models with dry sand on Vibrostol (without massive high -precision pressing machines, shaking, assemblies of forms, pneumatic reference, runners). The focus of attention was transferred to the production of models (these “lightest white toys” with a density of 25-27 kg/cubic meter), which is usually “trusted” by female hands, placing sites on the second and above the floors of buildings. Labor similar to the packaging displaces the image of the foundry, like a small mine.
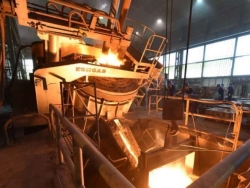
The revolutionary cooling of the sand after rash from the forms is carried out in passage cooler - in air -flow or drum, as a rule, mounting them with bunkers outside the workshop (sand is not afraid of frost). For black and colored alloys, the same domestic equipment is used (in contrast to traditional forming with the binder, when high -quality equipment is imported to it). So they receive castings from cast iron and became all types, bronze, brass and aluminum of all brands. In a box on a “Christmas tree or a bush” dozens of castings immediately pour, as in jewelry production.
Workshops and sites with this flexible technology are rapidly multiplying around the world - from America to China, in auto and instrumentation, Ford Motors, Fiat, General Motors, etc., several hundred patents for inventions - and their stream grows. Today, in the world, it produce castings of ~ 1.5 million tons/year, forecasts for the near future give this technology 10-20% of world casting. The Institute of FIMS, Kyiv (FCHPF Department of Prof. Shinsky O. I.), improving the "branded" specialization in this matter, designed equipment and launched a number of shops in Ukraine, Russia, Poland and Vietnam.
Low costs for model -forming materials (1 ton of fitness consumes four types: quartz sand - 50 kg, anti -tips - 25 kg, polystyrene foam - 6 kg and polyethylene film - 10 sq.m., no in the binder sand) save at least 100 dollars/t of casting along the entire volume of the container. 70-80%, savings in the width of metal by 250-300 kg, electricity 100-150 kWh, masses of castings by 10-20% compared to traditional outrageous molding. Large savings are casting complex castings of wear -resistant steels (screws for brick production machines, beats, hammers and parts of crushers), because the costs of their mechanical processing are sharply reduced. There are no restrictions on the configuration of castings.
The experience of launching plots up to 50-150 t/month showed the payback period up to 2 years, a set of equipment for shops of 10-80 tons/month is not much different. If we create or reconstruct the foundry, then casting by GAZMODELS - the business where the metal is transferred to its equipment and labor